Bespoke Leather Accessories
Small leather goods engineered on three numbers — yield per hide, coats of edge paint and stitches per inch — because those decide cost and service life.
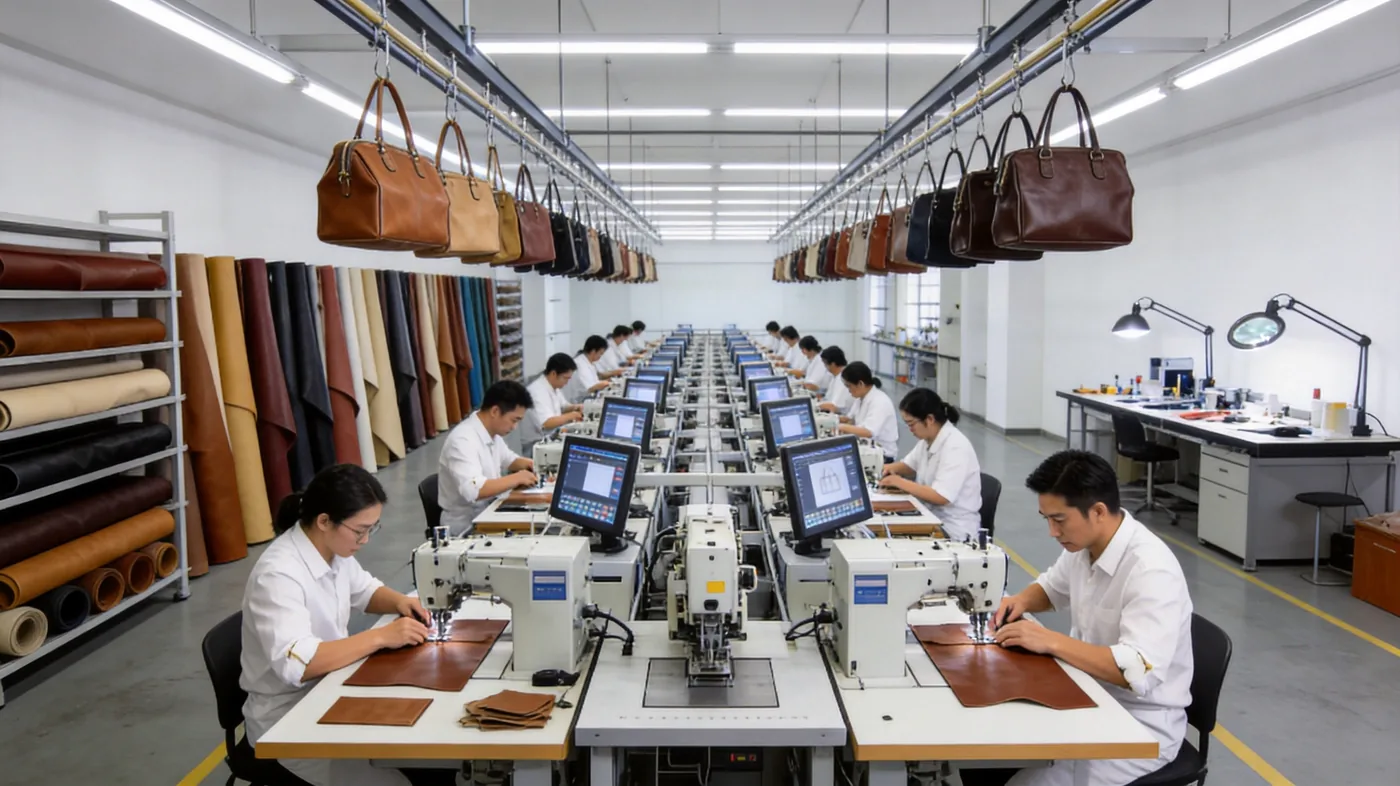
Leather accessories are small goods — card wallets, key cases, belts, passport covers, luggage tags, valet trays and flat pouches — developed to a stated leather, a stated construction and a stated edge finish, where yield planning and edge work decide whether a piece survives daily handling. Programmes start at 500 pieces per style and colourway; prototypes take 6–10 working days, 12–15 with custom hardware; bulk completes 35–50 days after approval. Lots release on AQL 2.5, ISO 2859-1, general level II, FOB Xiamen.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
Cutting Yield: Getting Small Parts Out of a Hide
On a handbag, leather cost is absorbed into a large panel and a modest waste figure. On a card wallet it is not: the panels are tiny, the perimeter is long relative to the area, and a hide is an irregular shape with graded zones. A full bovine hide averages 45 to 55 square feet, of which roughly 80 to 88 per cent survives grading once scars, brand marks and the low-density belly are excluded. Nesting small panels into that usable area typically returns 62 to 72 per cent.
That spread is worth real money across a 500-piece order. Nesting is therefore planned before the first hide is cut, and it is planned against the graded zones rather than against a flat rectangle: firmer material goes to belt straps and structured panels, softer flank goes to linings and pocket bags, and the belly is avoided entirely on any piece that takes a crease.
Substance selection interacts with the nest. Ordering 1.2 mm leather for a piece that only needs 0.9 mm does not make the piece better; it makes it stiffer, heavier and slower to skive, and it reduces the number of panels a hide will yield because more material is trimmed away at the folds. We set the substance per item from what the piece has to do — hold a crease, take an emboss, resist a pocket — and then nest to that figure.
| Item | Closed size | Panel count | Leather substance | Yield per 50 sq ft hide |
|---|---|---|---|---|
| Card wallet, four slots | 10 × 7 cm | 5 panels plus 2 pocket strips | 0.8–1.0 mm | 190–230 pieces |
| Key case, six hooks | 6.5 × 10 cm | 2 panels plus a hardware bar | 1.0–1.2 mm | 210–250 pieces |
| Passport cover | 10 × 14 cm | 2 panels plus 2 corner pockets | 1.0–1.2 mm | 120–150 pieces |
| Belt strap, 35 mm | 90–120 cm long | 1 strap, 1 keeper, 1 tip | 3.0–3.5 mm or two plies laminated | 14–18 pieces |
| Valet tray, riveted corners | 24 × 16 cm | 1 body blank, 4 corner wraps | 1.4–1.6 mm | 34–42 pieces |
Edge Paint, Skiving and Stitch Density
Three operations separate a small good that looks right on day one from one that still looks right after a year in a pocket. Skiving thins the leather where it folds or butts, so the build does not bulk at the seam. Edge paint seals the exposed fibre at every perimeter. Stitch density sets how the seam behaves when the piece is flexed. All three are specified on the tech pack, because all three are visible at arm's length.
| Edge treatment | Build-up | Cost index | Suited to |
|---|---|---|---|
| Turned edge | Edge skived to 0.6 mm over a 12 mm width, folded and stitched | 100 | Wallets and passport covers at the top of a range |
| Multi-coat edge paint | Three coats at roughly 0.15 mm each, sanded between coats | 78 | Volume programmes needing a clean, uniform line |
| Raw burnished edge | Edge sanded, dampened and slicked with a gum or wax finish | 62 | Vegetable-tanned leather and heritage-styled pieces |
| Bound edge | A 10 mm leather or fabric binding stitched over the perimeter | 85 | Pieces in suede or nubuck, where paint will not hold |
Thread and needle follow the stitch count. A bonded nylon or polyester in the Tex 40 to Tex 69 range, run through a 90/14 or 100/16 needle, gives a consistent loop at seven to nine stitches per inch on leathers of this substance. Thinner thread at a higher count reads finer and wears faster; thicker thread at a lower count reads heavy and can pucker a 0.8 mm panel. The pairing is stated on the tech pack so it is reproducible across re-orders.
Card Wallets, Key Cases, Belts and Passport Covers
Each item type has one specification that dominates everything else. On a card wallet it is slot geometry: a slot cut 2 mm narrower than a card will grip when new and loosen to useless in a month, while a slot cut 4 mm wider lets a card ride proud of the mouth. On a key case it is the hook bar, which takes the whole load. On a belt it is substance and hole pitch. On a passport cover it is corner pocket depth, which decides whether the booklet sits square.
- Card slots — cut with 3 mm of ease across the card width, with the mouth reinforced and the slot bottoms bar-tacked against splitting.
- Key hardware — a four- or six-hook bar riveted through a doubled panel, with the rivet load spread on a backer rather than through a single leather ply.
- Belt straps — 3.0 to 3.5 mm full-grain or two plies laminated to 3.2 mm, five holes at a 25 mm pitch, with a stitched keeper.
- Passport corners — pockets cut 3 mm below the booklet edge so the cover closes square and the corners do not curl.
- RFID shielding — a foil interlayer adding roughly 0.25 mm to the build, accounted for in the pattern rather than inserted afterwards.
- Stitch specification — 7 to 9 stitches per inch in a bonded nylon or polyester thread, with the count stated rather than left to the operator.
Lining is where small goods quietly gain bulk. A wallet lined in a heavy pig suede reads well in the hand and adds roughly 0.4 mm per internal layer, which across four card slots and two pockets is enough to stop the piece closing flat. A microfibre or a lightweight sheepskin lining gives most of the tactile benefit at half the build-up. Lining choice is therefore made with the closed thickness in mind rather than on the swatch alone.
Designing a Coherent Family of Small Goods
A family works when four things are held constant across every piece: the leather lot, the thread colour, the hardware finish and the brand-mark scale. Holding a fifth — the edge treatment — is what makes the family read as deliberate rather than merely coordinated. Holding them is easier on small goods than on bags, because the pieces are cut from the same hides in the same session, which is the practical argument for developing a wallet, a key case and a valet tray as one order rather than as three.
- Agree the item list and the price ladder first; a family of four reads better than a family of twelve.
- Choose one leather and one lining family, then let the items vary on substance rather than on finish.
- Fix the hardware finish — buckle, hook bar, rivets, snap, zip pull — across the whole family.
- Set the brand-mark scale per item; the mark that suits a valet tray will overwhelm a card wallet.
- Approve edge finish and stitch count on one prototype and apply the approved figures to every piece.
- Plan set packing at specification stage if the family is sold as a gift box.
Sets introduce one problem that single items do not: a gift box is a fixed volume, and the pieces inside it have to fill it convincingly without being forced. Where a family is sold boxed, the box is specified from the assembled set rather than bought from a catalogue, and the item count is chosen so the set reads as generous at the intended price. That decision belongs with the item list, not with the packaging order.
Sampling Sequence for Small Leather Goods
A first build is reviewed in the hand rather than on a bench. The questions are whether the slot grips a card without resisting it, whether the edge paint is even along the whole perimeter, whether the piece lies flat rather than cupping, and whether the emboss reads at arm's length. None of those are visible on a drawing, and all of them are visible on a finished piece held at arm's length.
Plated hardware is the other schedule risk. A cast buckle or a shaped fob has to be tooled, cast, tumbled and plated, and the plating bath is shared across jobs rather than dedicated to one order. A finish that is unusual for the region — a dark gunmetal, a brushed palladium tone, a two-tone treatment — can add a fortnight while the line is set up for it. Where the schedule is tight, choosing a finish that is already running is worth more than choosing the one that looks best on a moodboard.
The second build is cut from bulk leather with bulk hardware and becomes the sealed reference. Where custom metal work is involved — a cast buckle, a shaped fob, a plated hook bar — that component governs the schedule rather than the leather, and it is worth commissioning it early rather than discovering in week four that the plating bath is the critical path.
Acceptance Criteria and Long-Term Care
Small goods release on AQL 2.5 under ISO 2859-1, single sampling, general level II, and the weighting follows the defect categories that actually occur here — edge coverage, stitch consistency, emboss registration and slot geometry — rather than the load-bearing checks that dominate bag inspection.
- Edge examination — coverage, adhesion and colour match against the sealed sample, checked on every pulled unit.
- Stitch count — stitches per inch verified on the seam, with seam straightness measured against the panel edge.
- Slot and pocket function — a card inserted and withdrawn repeatedly on pulled units to confirm grip without resistance.
- Crocking and colour fastness — leather and linings rub-tested dry and wet, particularly on saturated colourways.
- Compliance — REACH (EC) 1907/2006 and CPSIA declarations; OEKO-TEX Standard 100 linings and LWG-sourced leather on request.
- Production floor — an SGS-verified 4,950 m² site in Quanzhou, Fujian running 7 lines and 149 machines with 137 staff.
Hardware Selection for Small Goods
Hardware on a small good carries a different kind of load than hardware on a bag. A tote distributes weight across a handle root and a panel; a key case puts the entire contents of a pocket onto six hooks and two rivets, and a belt puts sustained tension through a buckle fold every time it is worn. Because the leather around the fixing is thin, the failure is rarely the metal itself — it is the leather tearing away from it. Specifying hardware therefore means specifying what sits behind it.
| Component | Load it actually takes | Common failure | Specification response |
|---|---|---|---|
| Hook bar, four or six hooks | Static weight of keys, plus a twisting pull as the case is opened | Hooks spreading and the bar loosening in the panel | A bar riveted through a doubled panel with a backer spreading the rivet load |
| Rivet, valet tray corners | Repeated flexing each time the tray is flattened or folded | Rivet pulling through a single ply | A washer or backer on the reverse face and a corner wrap cut on the bias |
| Snap closure | Daily opening cycles, typically several hundred a year | Socket working loose in thin leather | An eyelet-reinforced seat and a cap chosen for the substance, not the look |
| Buckle, belt strap | Sustained tension at the hole and at the fold | Hole elongation and creasing at the fold | A 3.0–3.5 mm strap or two-ply lamination, with the fold stitched rather than riveted alone |
| Zip, flat pouch | Lateral pull along a short, unsupported run | Tape separating from a skived edge | A bound or turned edge at the tape seat and a stop bar-tacked through both plies |
Finish is the second decision and it has a schedule consequence. Cast and plated components share a plating bath across jobs, so a finish that is already running on the line arrives quickly while an unusual tone — a dark gunmetal, a brushed palladium, a two-tone treatment — waits for the bath to be set up. Choosing a running finish is usually the single largest saving available on a small goods schedule, and it costs nothing in appearance when the family was always going to be coordinated.
Weight is the trade-off to watch. A solid brass component has the right feel and the right wear pattern, but on a card wallet it adds noticeable mass to a piece that lives in a pocket, and it can pull a thin panel out of flat. A zinc alloy of the same geometry and finish costs less and weighs less, and on a piece this size the difference is rarely detected by the customer. Reserve solid brass for belt buckles and larger fobs, where the weight reads as substance rather than as burden.
Retail-Ready Packing and Presentation
Small goods are handled differently from bags at the retail end. They are picked up, turned over, and often bought as gifts, which means the packing has to survive being opened more than once and has to read as considered at close range. The specification decisions that matter here are mostly about restraint: fewer elements, chosen well, outperform a stack of printed inserts.
- Dust bag — natural cotton or a non-woven alternative, sized to the closed piece with enough ease that it can be removed and replaced without snagging an edge.
- Rigid or semi-rigid box — specified from the assembled set where pieces are sold boxed, so the contents fill the volume without being forced in.
- Care card — printed on uncoated stock, carrying the leather type, the tanning route and the two or three care actions that actually extend service life.
- Barcode and labelling — retail labelling applied at packing rather than at the piece, so a change of retailer does not require reworking the goods.
- Set assembly — gift sets collated and checked as a unit, with a packing list verified against the set rather than against the individual item count.
- Carton specification — a carton chosen for the stacking height and humidity of the destination route, since small goods are light and cartons are frequently cubic-ed out before they reach weight limits.
One detail is worth planning early. Where pieces are sold through more than one channel, the only difference between them is often a label or a hang tag, and applying that at packing keeps the goods themselves identical. That preserves the option to redirect inventory between channels later, which on a 500-piece minimum is worth more than it sounds, and it avoids the cost of holding separate runs for each retailer.
Two packing decisions are worth settling while the specification is still open, because both are expensive to revisit. The first is whether the set is assembled at the production site or at the destination; assembling at the site means the set can be checked against a packing list as a unit and re-worked immediately, whereas destination assembly leaves a mismatch discoverable only after the cartons have landed. The second is carton cube: small goods are light, so cartons typically reach their volume limit long before any weight limit, and a slightly tighter fold on the box can change how many units fit a container.
Where the Money Goes on a 500-Piece Run
Small goods confuse buyers because the unit price looks high relative to the size of the object. The explanation is fixed cost: pattern engineering, nesting, tooling for any custom metal work, and line configuration are largely independent of how big the piece is. On a structured bag those costs spread across a large material and labour base; on a card wallet they spread across very little, so they remain visible in the unit price until volume climbs.
| Cost element | What moves it | Behaviour at 500 pieces |
|---|---|---|
| Leather | Substance, grade, tannery and the yield achieved in nesting | The largest variable line; yield planning is where it is won or lost |
| Hardware | Whether components are stock items or tooled, and the plating finish | Stock items are cheap; tooling and a non-running finish dominate |
| Labour | Edge treatment and stitch count, both driven by perimeter length | Higher than buyers expect relative to piece size |
| Pattern and sampling | Number of distinct items in the order | Falls per item sharply when several items are developed together |
| Packing | Box specification, set assembly and retail labelling | Modest alone, material when the set is boxed |
| Compliance testing | Market declarations required and whether dark colourways need crocking tests | Largely fixed, so it is a smaller share of a larger order |
The practical consequence is that the cheapest way to develop small goods is rarely to develop one item. Three or four pieces sharing a leather lot, a hardware finish and a sampling round amortise the fixed elements across the group, and because they are cut from the same hides in the same session they also hold colour consistency better than the same items ordered months apart. Programmes built this way typically land the whole family for noticeably less per piece than the sum of the items costed individually.
It is also worth asking what a larger run would actually change before assuming it will help, because the answer differs by cost line. Moving from 500 to 2,000 pieces improves the leather price through better hide purchasing and improves the fixed-cost spread, but it does not change labour per unit much, because edge work and stitching scale with the piece rather than with the order. The saving is real but it is not linear, and it is usually smaller than the cost of holding two years of inventory in a category where colourways go out of fashion quickly.
Reorders, Colourway Extensions and Range Growth
A small goods range rarely stops at its first order. The useful question to settle at the outset is what will make a reorder easy, because most of the difficulty in a second run comes from decisions that were never written down the first time: which hide lot matched, what the approved edge paint code was, and who signed off the emboss depth.
- Retain the sealed reference from the second build and store it against the style number, not against the purchase order.
- Record the hide lot, the edge paint code and the thread reference on the tech pack so a reorder can be matched rather than re-negotiated.
- Keep tooling against the style; cast buckles and shaped fobs are the components most often lost between orders.
- Treat each additional colourway as its own costed line, because a second colour repeats the fixed elements rather than sharing them.
- Sequence extensions from the approved standards outward — a new item on known leather first, a new leather second.
The order of extension matters more than the pace of it. A new item built on an approved leather is a low-risk addition; a new leather introduced across an existing range is not, because it reopens colour matching, edge paint compatibility and yield planning on every piece at once. Introducing one new item first and letting it validate the demand before committing to a second colourway keeps the risk on a single style.
Brands extending into adjacent categories usually start from the standards already approved here. Once a leather lot, a hardware finish and an edge treatment are signed off on a wallet and a key case, adding a structured handbag or a business bag to the same family costs less in development than starting a separate range, and the pieces read as one collection on shelf. The private label route suits brands that want those standards carried across a full assortment.
Brief a small leather goods programme
Send the item list, the leather direction and the target quantities. We will return a yield calculation, a costed specification and a schedule.
Frequently Asked Questions
How much does cutting yield really move the unit price on a card wallet?
Materially. A graded-zone nest on a 50 square foot hide returns roughly 190 to 230 four-slot wallets; a naive flat-rectangle nest loses 8 to 12 per cent against that. Across a 500-piece order the difference is several hides, and because small goods have long perimeters relative to their area, waste is a larger share of cost here than on any structured bag.
Why is a belt specified at 3.0 to 3.5 mm rather than the 1.2 mm used elsewhere?
A belt takes sustained tension at the holes and at the buckle fold, and a thin strap rolls and creases under that load. Substance is achieved either by cutting a single 3.0 to 3.5 mm full-grain strap, which is expensive and increasingly hard to source, or by laminating two thinner plies to roughly 3.2 mm, which is the more common and more stable route.
How many coats of edge paint are applied, and why?
Three coats at roughly 0.15 mm each, sanded between applications. A single heavy coat bridges and then cracks along the fibre edge; three thin coats build a film that flexes with the leather. Edge cracking is the most common cosmetic failure on small goods, and it is almost always a coating-thickness problem rather than a paint-quality problem.
Can slots and pockets be tested before the bulk run?
Yes. Cards are inserted and withdrawn repeatedly on prototype and pulled units to confirm the mouth grips without resisting, and pocket depth is checked against the actual booklet or device the piece is built around. Slot geometry is the sort of specification that looks correct on a drawing and is wrong in the hand, so it is always checked physically.
Does RFID shielding change how the piece is built?
It adds roughly 0.25 mm to the build and slightly stiffens it, which changes how a wallet closes and how a passport cover sits flat. The shielding layer is therefore accounted for in the pattern rather than slipped in during assembly, and the pre-production sample is built with it so the closure behaviour is approved as it will actually ship.
How is the brand mark scaled across items of very different sizes?
The mark is sized per panel rather than taken from a logo sheet at one scale. A mark that sits well on a 24 × 16 cm valet tray will overwhelm a 10 × 7 cm card wallet, so each item gets its own die size in proportion to its panel, while the position rule and the depth stay constant across the family.
What is the best entry item for a first small goods programme?
A card wallet or a key case. Both are simple enough that the first prototype is usually close, both share a leather lot and a hardware finish with anything developed later, and both give a brand an accessible price point. A valet tray or a belt is better added second, once the leather and finish standards are already approved.
Do dark colourways need extra testing?
Yes. Saturated and dark leathers are the ones most likely to transfer pigment, so they are rub-tested dry and wet for crocking before release. Where a piece will sit against light-coloured clothing or upholstery, that test is worth commissioning explicitly rather than relying on the standard inspection, which may not cover it.
Can small goods be reordered in a single colourway years later?
Yes. The sealed reference, approved lab dips and tooling are retained against the style, so a reorder runs against the original specification without a second sampling round. The 500-piece floor applies again per style and colourway, which is the main reason programmes consolidate several items into one reorder rather than placing them separately.
Why does hardware fail on small goods more often than on bags?
Because the leather around the fixing is thin, so the metal is rarely what gives way — the panel tears away from it. The specification response is reinforcement behind the fixing: a backer spreading the rivet load, an eyelet-reinforced seat under a snap, and a bound or turned edge where a zip tape is seated. Hardware is therefore specified together with what sits behind it rather than on its own.
Does choosing a stock hardware finish really change the schedule?
Yes, and it is usually the largest single saving available. Cast and plated components share a plating bath across jobs, so a finish already running on the line moves straight through while an unusual tone waits for the bath to be prepared. Where a schedule is tight, selecting a running finish is worth considerably more than optimising the leather choice.
Why is the unit price on a card wallet high relative to its size?
Fixed cost. Pattern engineering, nesting, tooling and line configuration are largely independent of how large the piece is, and on a small good there is very little material and labour for them to spread across. The practical answer is to develop several items in one order so those fixed elements amortise across the group rather than landing on a single style.
Should retail labelling be applied to the piece or at packing?
At packing wherever possible. Applying barcodes and channel labels during packing keeps the goods themselves identical across retailers, which preserves the option to redirect inventory between channels later and avoids holding separate production runs. It also means a change of retailer does not require reworking finished pieces.